

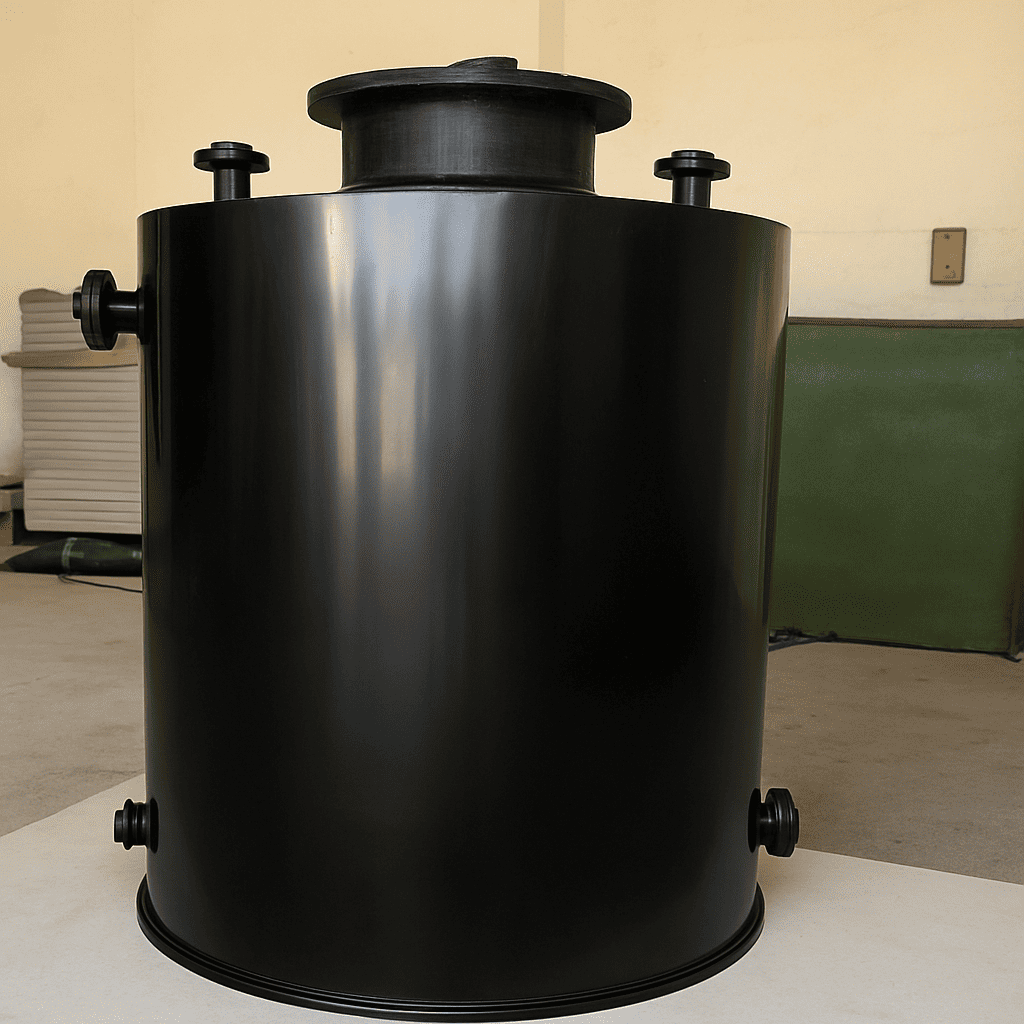
Polypropylene (PP) Tanks are engineered storage solutions designed for maximum durability, chemical resistance, and long-term performance. Manufactured using high-quality polypropylene, these tanks are ideal for handling corrosive chemicals, acids, alkaline solutions, and a wide range of industrial liquids.
Their lightweight yet robust structure makes them a preferred choice across industries such as chemical processing, pharmaceuticals, water treatment, electroplating, and food processing.
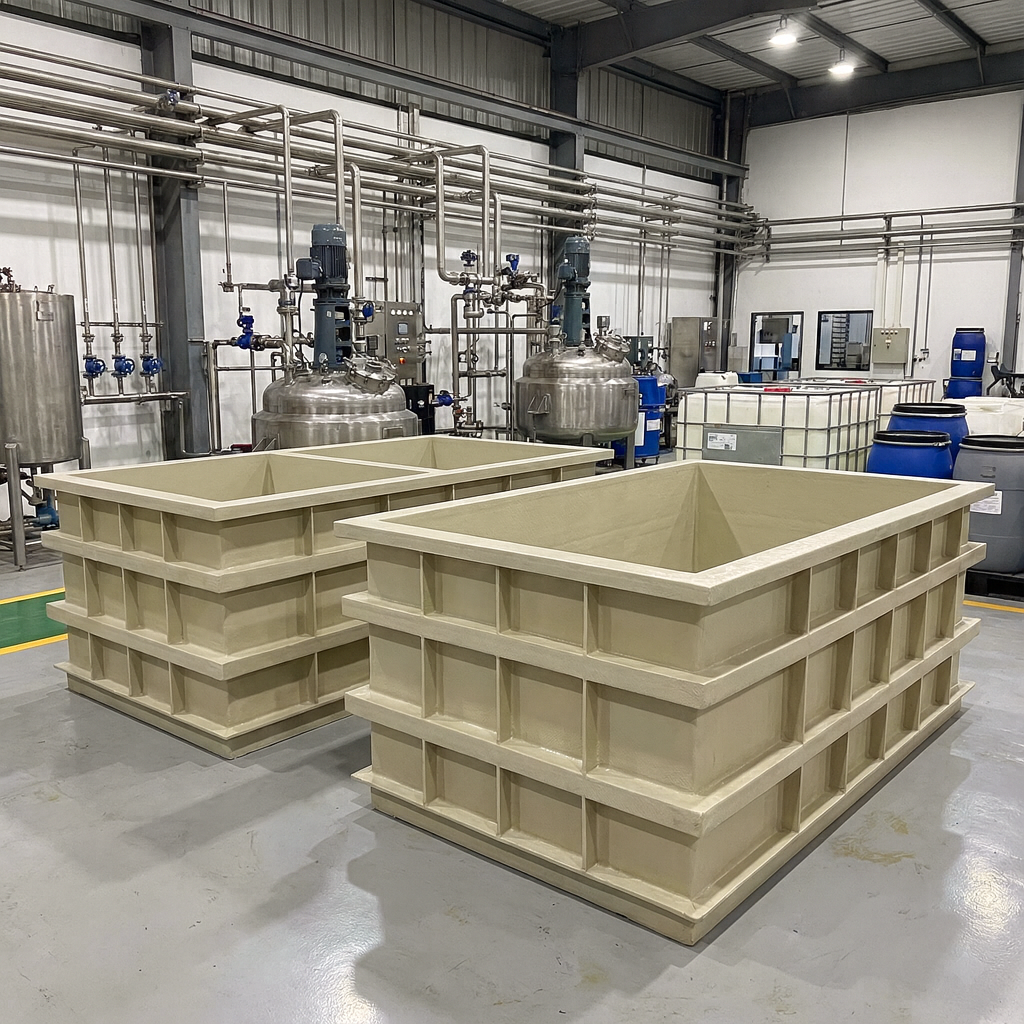
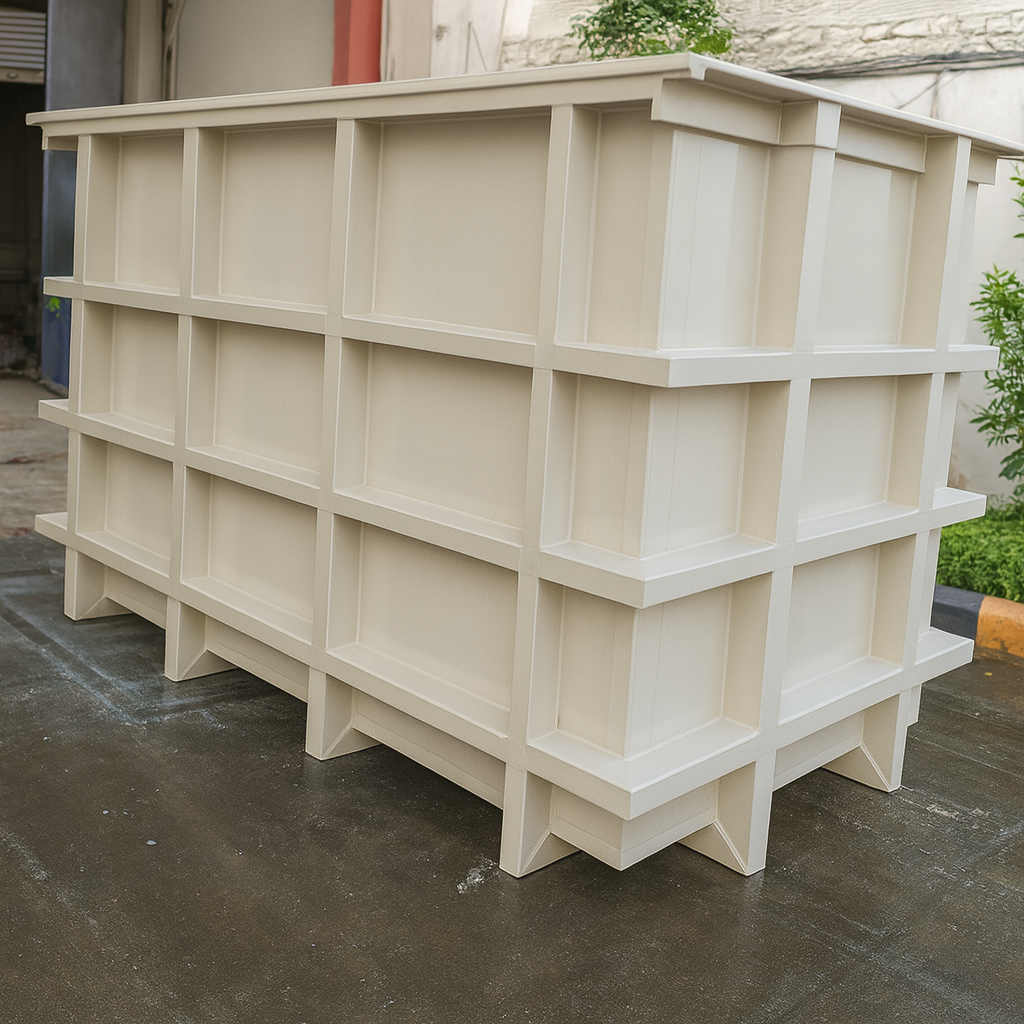
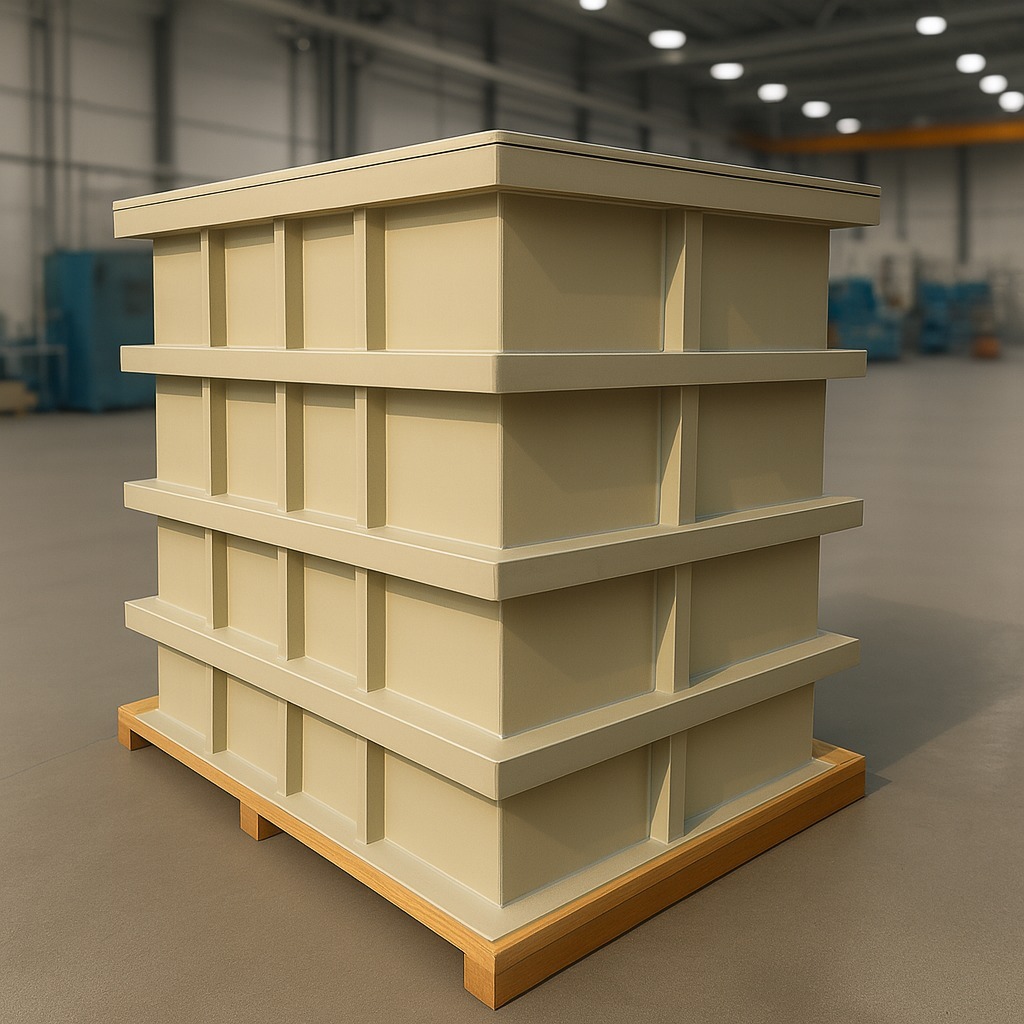
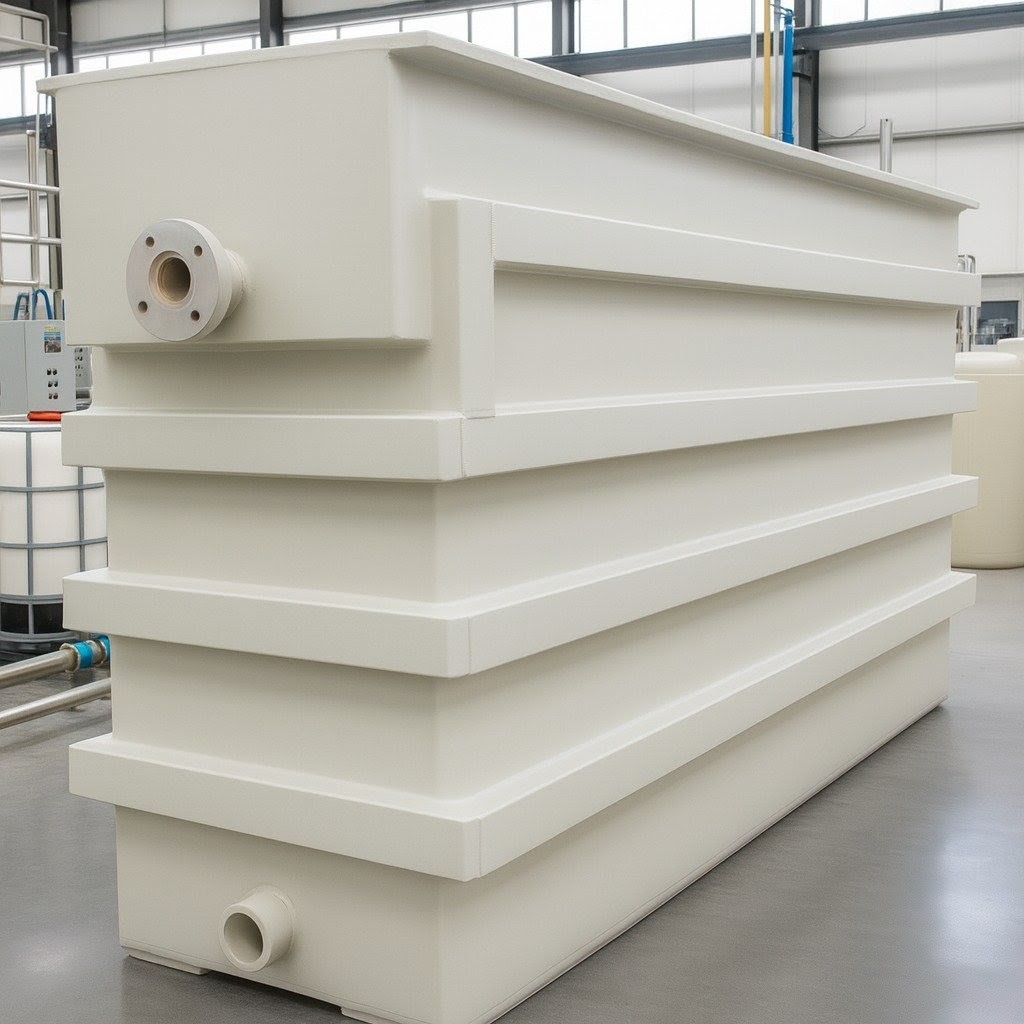
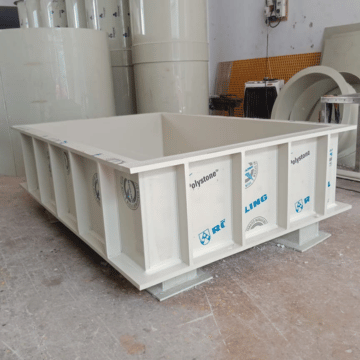
Ideal for storing corrosive chemicals, acids, alkalis, and aggressive industrial liquids in a safe and leak-proof manner.
Utilized in textile, dye, pigment, and paper industries for process chemical and liquid storage in production lines.
Widely used in chemical processing plants for safe chemical handling, dosing, and intermediate storage in various processes.
Effective for fertilizer, pesticide, and agro-chemical storage requirements in agricultural and allied sectors.
Suitable for effluent treatment plants (ETP), sewage treatment plants (STP), and RO/DM water systems for chemical and liquid storage.
Suitable for food-processing industries for handling non-reactive liquids where cleanliness and material compatibility are important.
Commonly used in pharmaceutical industries for hygienic, contamination-free, and easy-to-clean liquid storage applications.
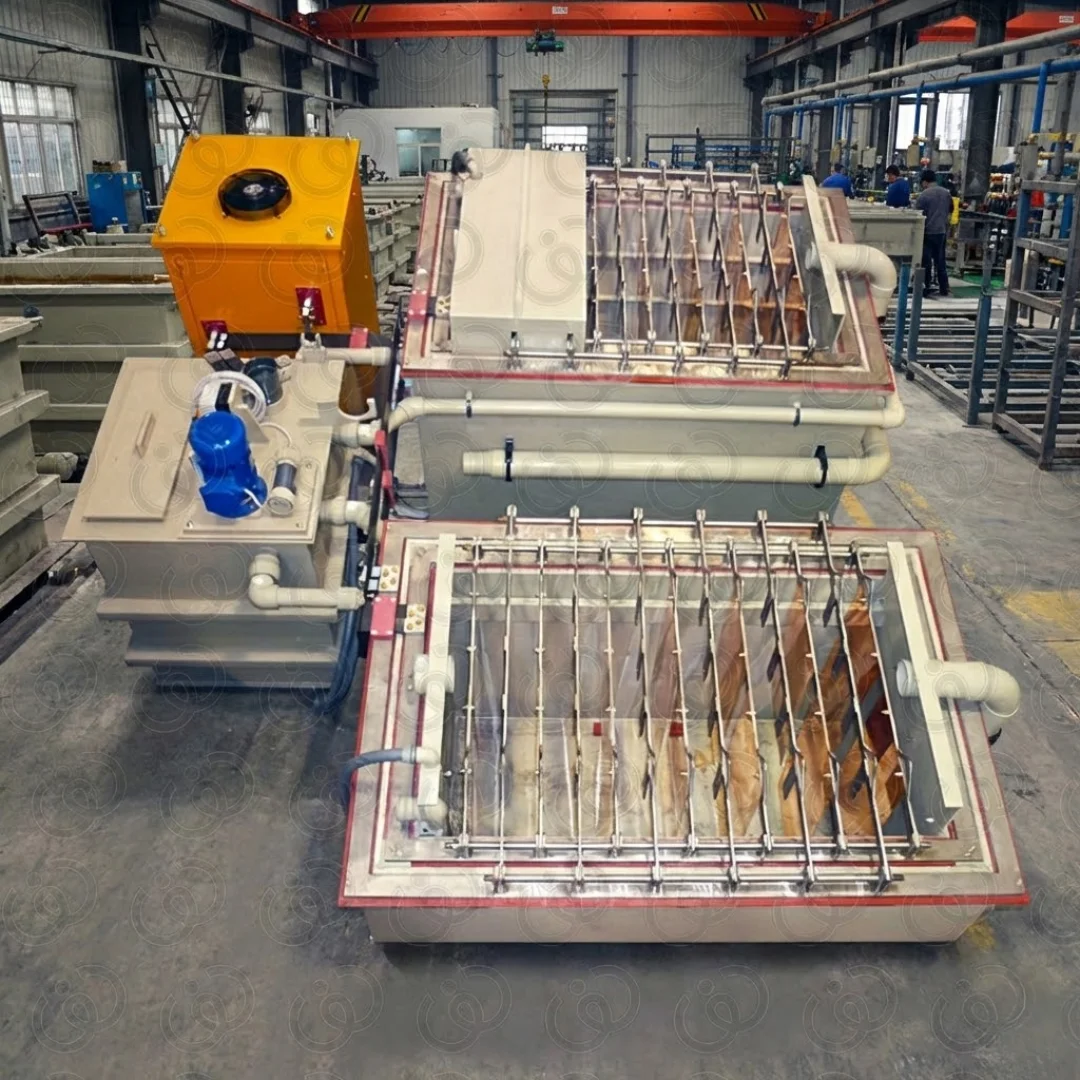
Used as reaction, mixing, neutralization, and buffer tanks in a wide range of industrial operations and processes.
Explore our premium PP, HDPE, FRP tanks and industrial equipment designed for durability, safety and performance.
Veer Technoplast Industries manufactures durable, corrosion-resistant industrial tanks, scrubber systems, and advanced plastic engineering solutions.
2026 All Rights Reserved | Website by IndustryLead
 Download Brochure
 Catalog


