

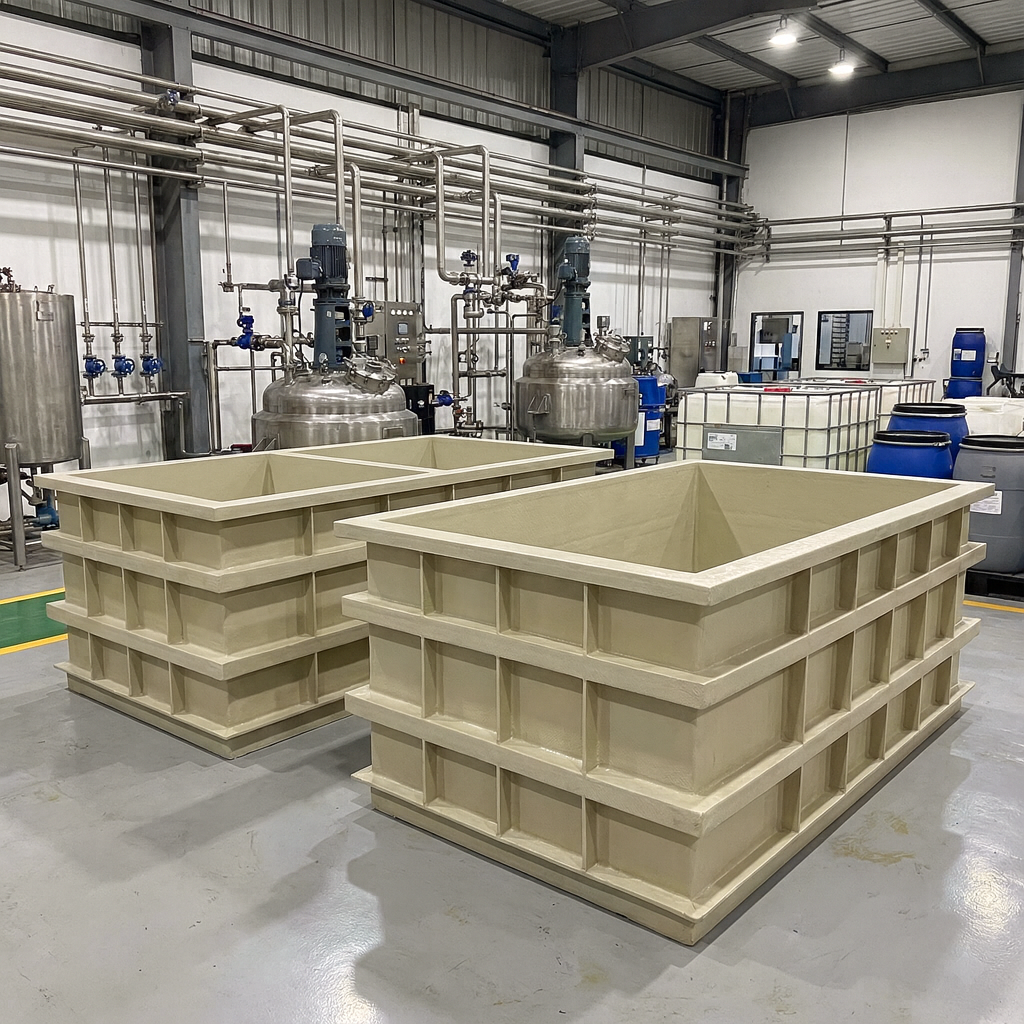
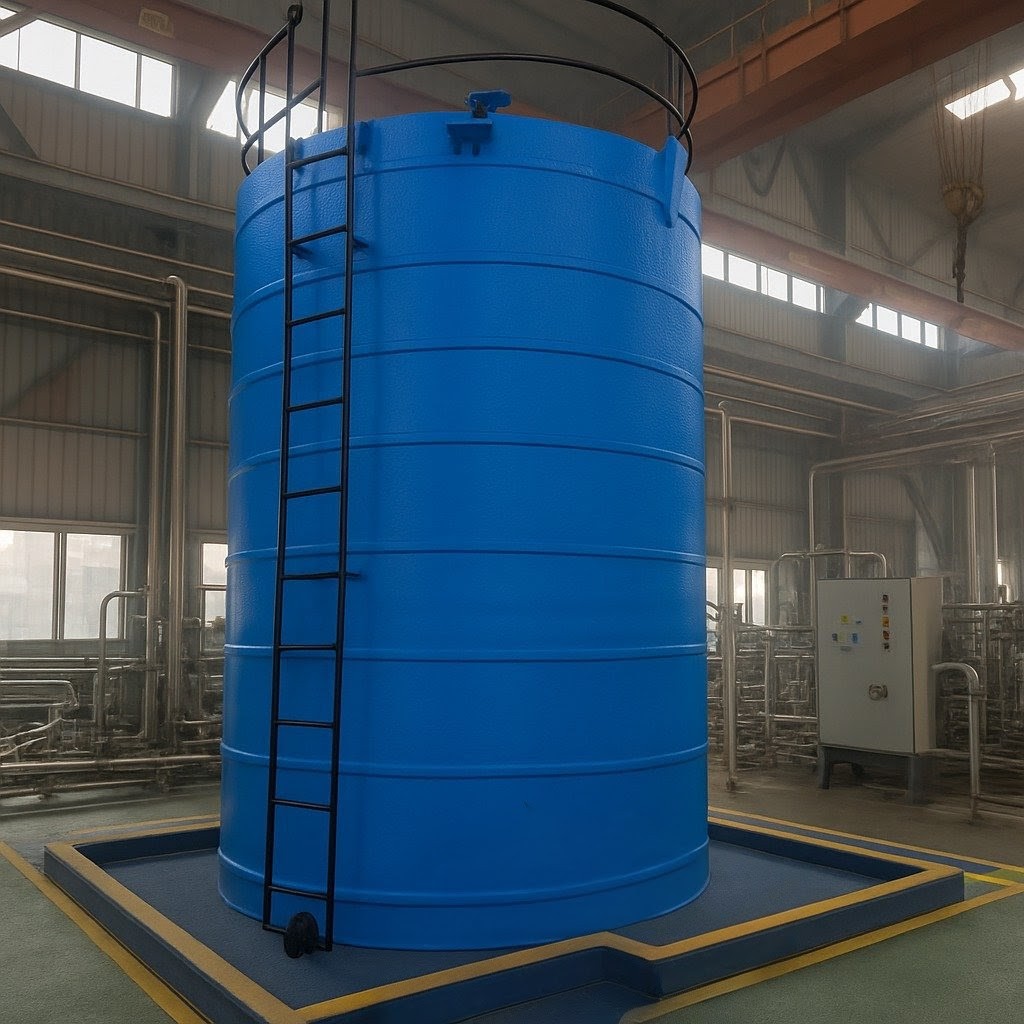
HDPE (High-Density Polyethylene) Tanks are engineered to provide reliable, long-lasting storage solutions for a wide range of liquids and chemicals. Lightweight yet highly durable, HDPE tanks deliver excellent performance in both indoor and outdoor environments.
They are UV-stabilized, maintenance-friendly, and designed to withstand harsh weather conditions. With flexible customization options in size, shape, and configuration, HDPE tanks provide a cost-effective, eco-friendly, and dependable solution for modern storage needs.
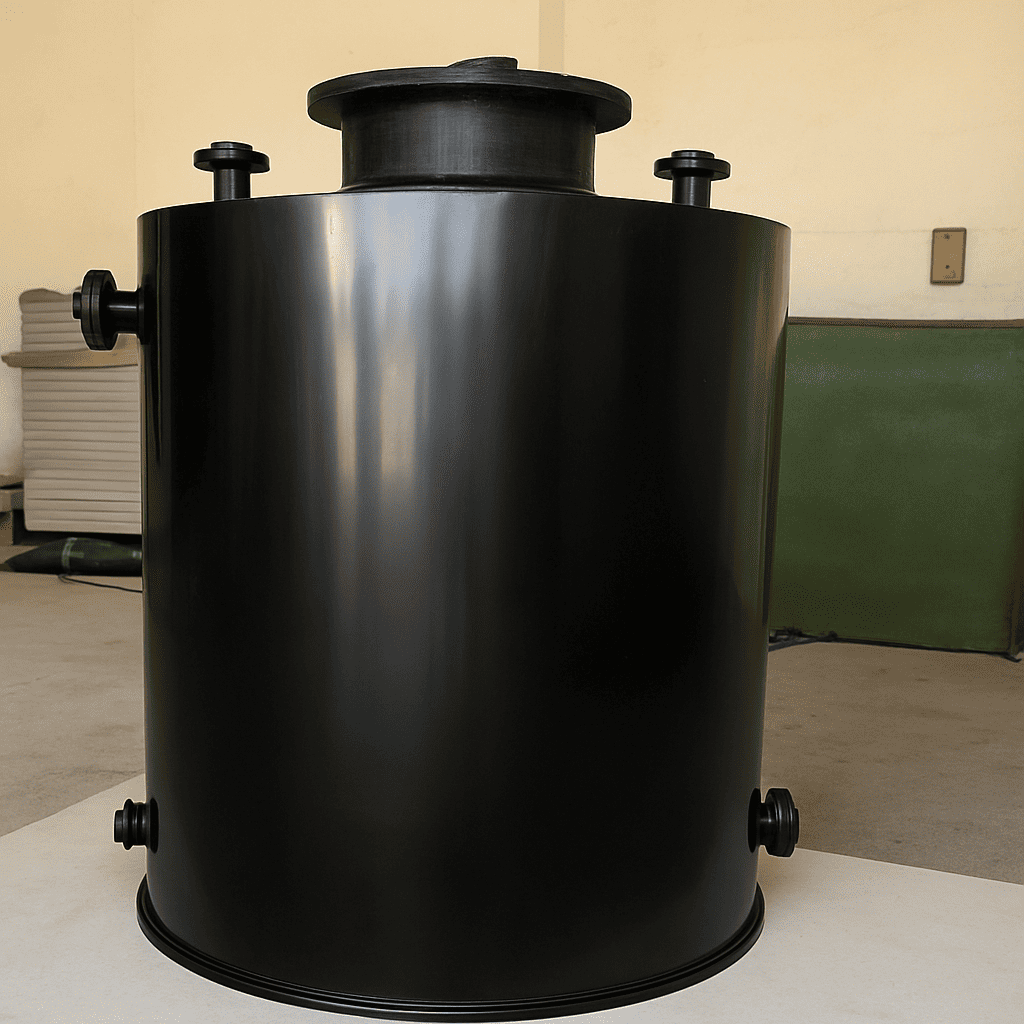
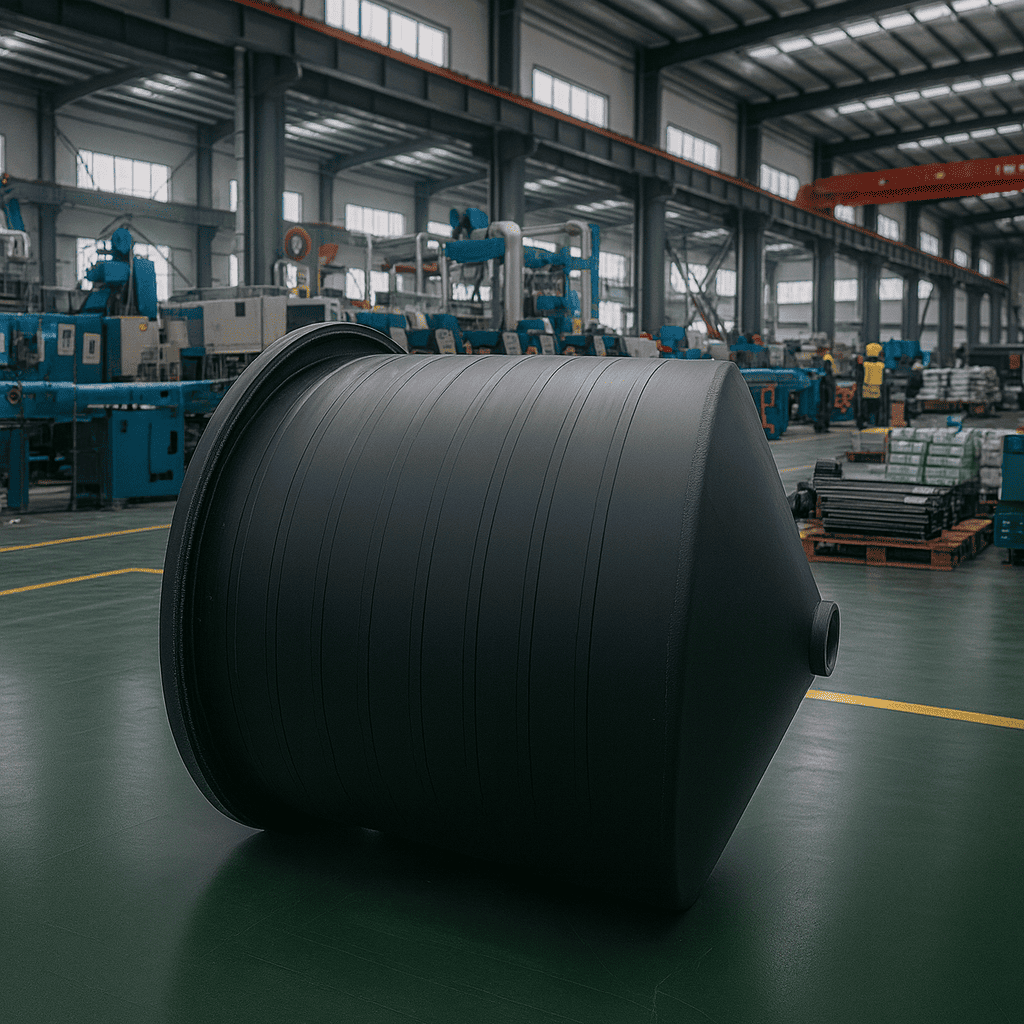
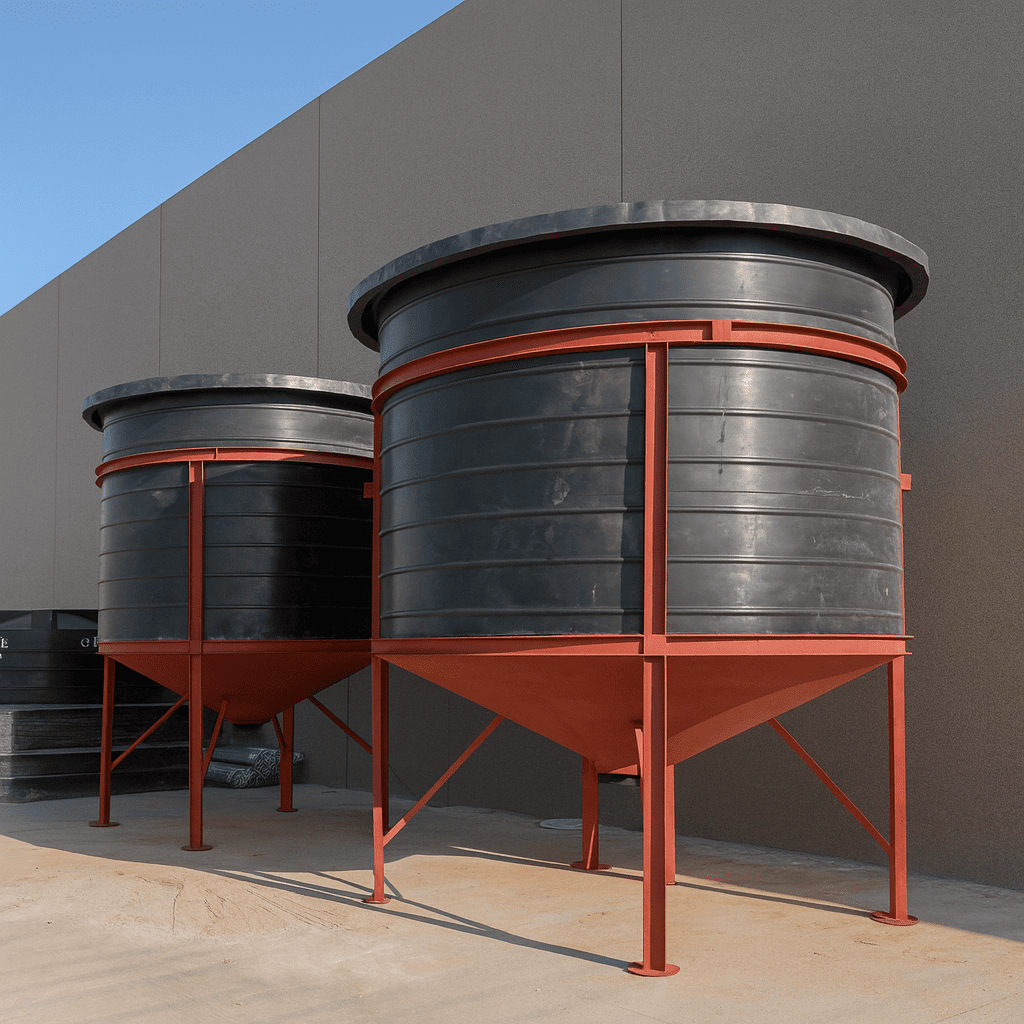
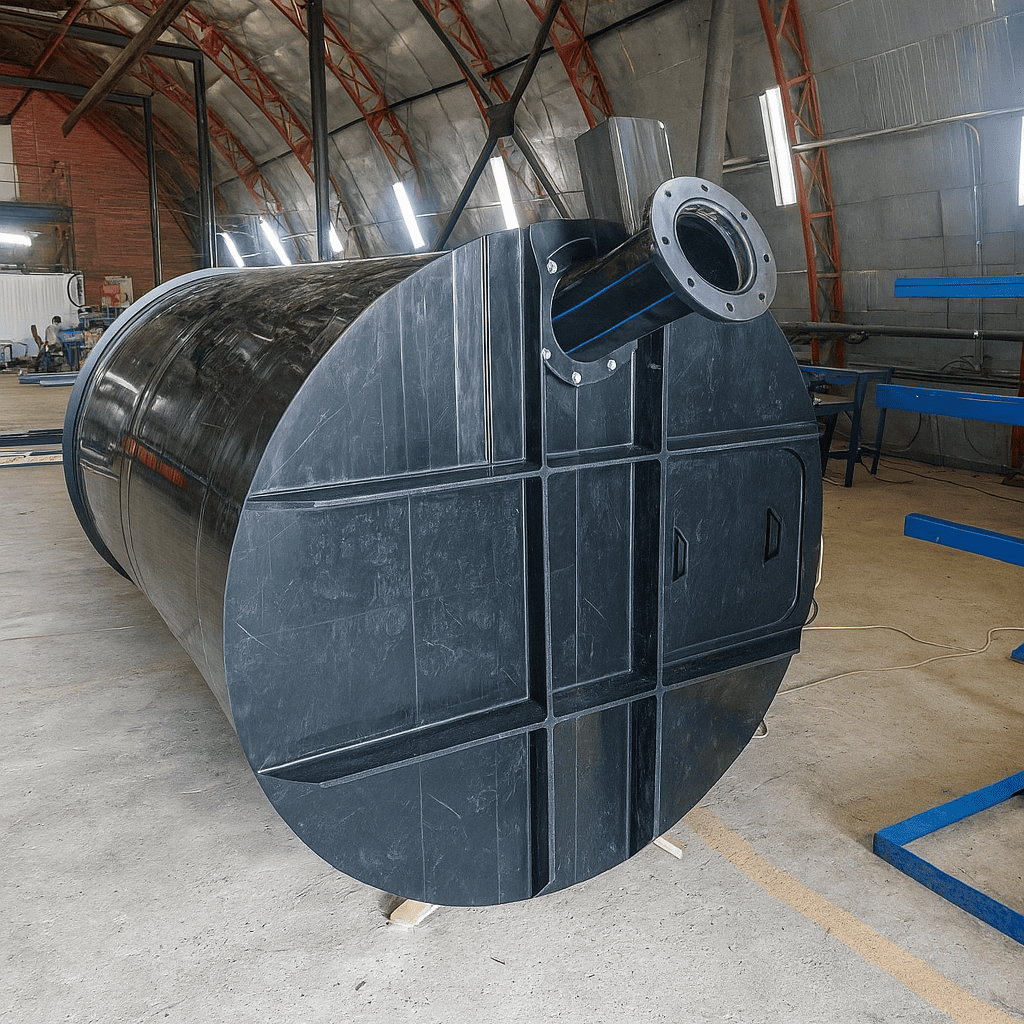
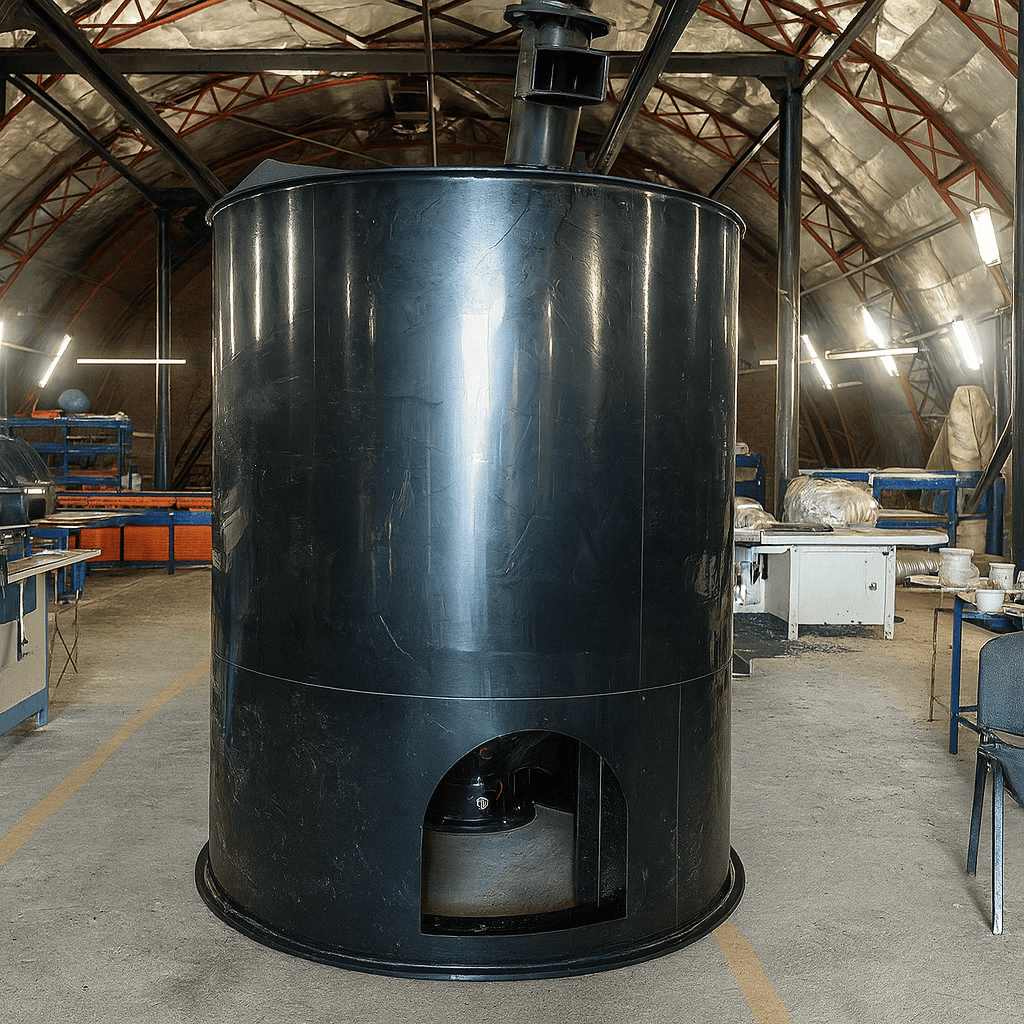
Ideal for safe storage of corrosive chemicals, acids, alkalis, and a wide range of industrial solvents without rust or leakage.
Effective for storage of fertilizers, pesticides, and agro-chemicals in liquid or solution form for agriculture and allied sectors.
Widely used in chemical processing plants for handling process liquids safely in continuous and batch operations.
Utilized in mining operations for containment of slurry, solutions, and reagents used in ore processing and treatment.
Suitable for water treatment facilities including RO, DM, ETP, and STP systems for storing treatment chemicals and process liquids.
Suitable for textile, dye, and paper industries for storage of liquid dyes, sizing agents, and other process chemicals.
Used for storing process water, raw water, and treated wastewater in industrial and utility applications.
Used as mixing, batching, or reaction tanks in industrial plants where chemical compatibility and durability are critical.
Explore our premium PP, HDPE, FRP tanks and industrial equipment designed for durability, safety and performance.
Veer Technoplast Industries manufactures durable, corrosion-resistant industrial tanks, scrubber systems, and advanced plastic engineering solutions.
2026 All Rights Reserved | Website by IndustryLead
 Download Brochure
 Catalog


