
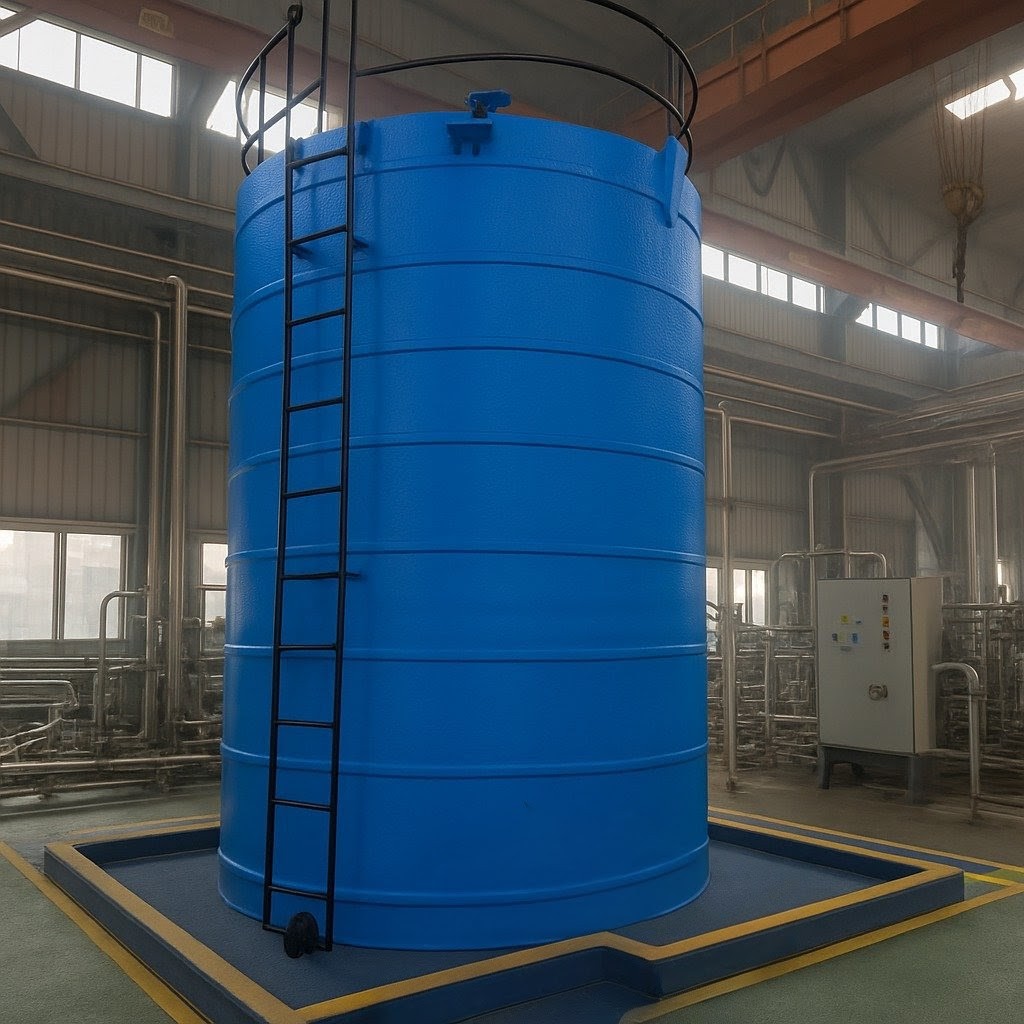
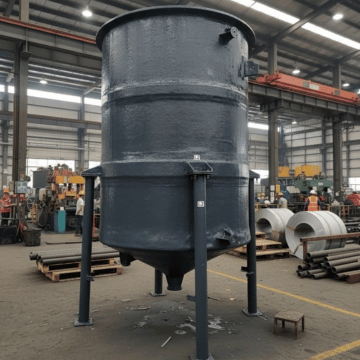
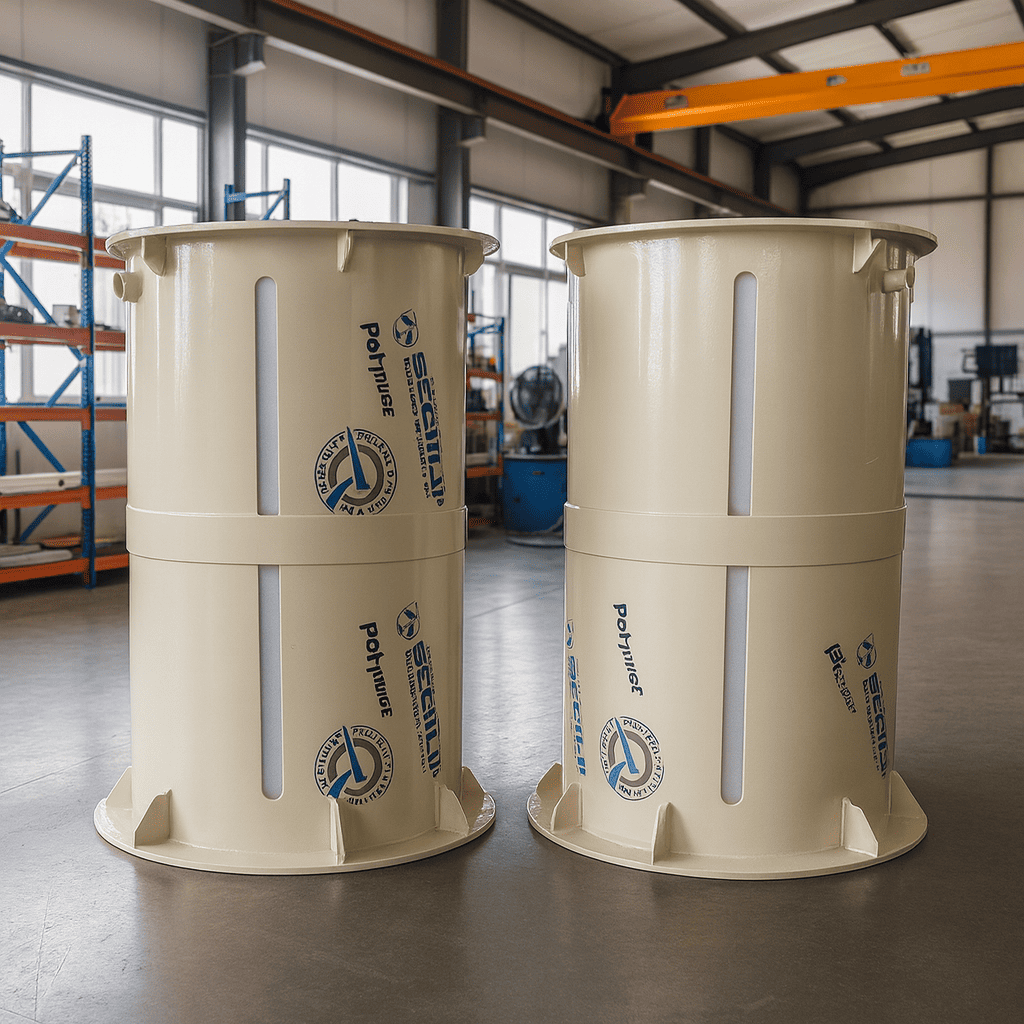
FRP (Fiberglass Reinforced Plastic) and FRP + PP (Polypropylene Lined FRP) Storage Tanks are advanced, high-performance solutions designed for the safe and efficient storage of corrosive and non-corrosive liquids.
Engineered with a combination of reinforced fiberglass and, when required, a chemical-resistant PP inner lining, these tanks offer superior structural strength, outstanding corrosion resistance, and long-term durability even in the most demanding industrial environments.


Ideal for storing corrosive chemicals, acids, alkalis, and industrial solvents in harsh environments where resistance to corrosion is critical.
Perfect for electroplating, anodizing, pickling, and other metal-treatment operations involving chemically aggressive solutions.
Widely used in chemical processing industries for safe containment and handling of hazardous liquids in various production processes.
Utilized in fertilizer, pesticide, and agro-chemical manufacturing and storage facilities for reliable containment of liquid products.
Suitable for effluent treatment plants (ETP), sewage treatment plants (STP), and wastewater management systems for liquid and chemical storage.
Commonly used in food-processing, beverage, and dairy industries for handling non-reactive liquids in hygienic conditions.
Used in pharmaceutical and biotechnology units for contamination-free, hygienic liquid storage where cleanliness and product safety are essential.
Well-suited for textile, dye, pigment, and paper industries in chemical storage applications across various stages of production.
Explore our premium PP, HDPE, FRP tanks and industrial equipment designed for durability, safety and performance.
Veer Technoplast Industries manufactures durable, corrosion-resistant industrial tanks, scrubber systems, and advanced plastic engineering solutions.
2026 All Rights Reserved | Website by IndustryLead
 Download Brochure
 Catalog


